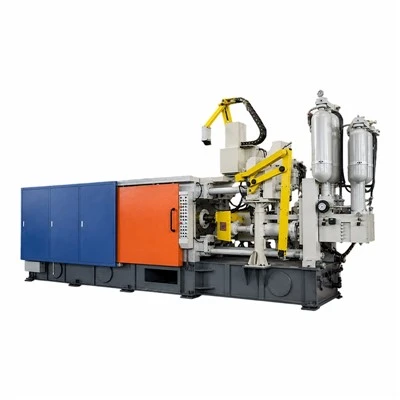


Ultra-Large Die Casting Machine
The Challenge of Macro-Structural Casting
Manufacturing an entire vehicle frame in a single cycle alters the fundamental physics of casting. When pushing molten metal across vast mold dimensions, the fluid must reach the furthest extremities before it begins to cool and solidify. A microsecond delay in hydraulic thrust results in cold shuts, instantly turning a massive structural component into scrap. Furthermore, the extreme expansion forces generated inside these gigantic molds will warp standard platens, destroying tooling that costs millions to produce.
Nantong HengMing Machinary engineers equipment specifically to handle these brutal macro-structural realities. By integrating world-class Siemens logic processing and heavy-duty Rexroth manifolds, this ultra-large die casting machine executes massive fluid volume delivery without pressure degradation. Coupled with reinforced cast-steel platens designed to maintain absolute parallelism, it secures the dimensional accuracy required by global automotive manufacturers.
Technical Specifications
|
Specification |
Unit |
HM-C2000 |
|
Die locking force |
KN |
20000 |
|
Inner space between tie bars(H*V) |
mm |
1350*1350 |
|
Die thickness (min-max) |
mm |
650-1600 |
|
Die stroke |
mm |
1400 |
|
Ejection stroke |
mm |
300 |
|
Ejection force |
KN |
650 |
|
Injection force |
KN |
1500 |
|
Injection position |
mm |
0,-350 |
|
Injection stroke |
mm |
1000 |
|
Diameter of pressure chamber |
mm |
130-170 |
|
Weight of feeding metal per time (AL) |
kg |
42 |
|
Casting projected area |
Cm2 |
1770-5000 |
|
Circle period |
s |
25 |
|
Pipe line pressure |
Mpa |
14 |
|
Motor power |
kw |
55*2 |
|
Oil tank capacity |
L |
3000 |
|
Machine weight |
kg |
140000 |
|
Overall dimension(L*W*H) |
m |
14*4.2*4.5 |
Extended Flow Length Management
Different lightweight metals exhibit vastly different thermodynamic behaviors over long distances. Magnesium, for example, loses temperature rapidly. To prevent premature solidification, the hydraulic architecture must deliver aggressive, sustained velocity. This capability makes the equipment an exceptionally reliable magnesium die casting machine for aerospace and automotive weight reduction projects.
Conversely, structural aluminum requires immense terminal packing pressure to eliminate internal porosity in thick-walled nodes. The heavy fluid dynamics allow this system to function as a powerful aluminum alloy die casting machine for infrastructure components. By mastering this extended flow length management, the equipment excels as a dedicated car body making machine and a unified body making machine for one-piece rear underbodies and battery enclosures.
Operating as a robust very large die casting machine, it provides the scale and stability necessary for:
Automotive Frames
One-piece chassis structures, shock towers, and battery housings.
Heavy Infrastructure
Large telecom base station heat sinks and architectural structural nodes.
Aerospace & Transit
Large interior framework panels and high-speed rail components.
Component Details

Caption:
The massive footprint of the equipment, specifically engineered to withstand the extreme expansion forces of macro-structural automotive casting.

Caption:
Heavy-duty cast steel platens designed to maintain strict structural parallelism under ultra-tonnage clamping loads.

Caption:
World-class Rexroth fluid manifolds delivering the massive hydraulic volume necessary for extended metal flow lengths.

Caption:
Verifying the macro-structural integrity of a large aluminum vehicle frame produced in a single injection cycle.
Macro-Structural Integrity Verification
Machinery of this scale cannot rely on theoretical load limits. Before the equipment is dismantled for logistics, it undergoes severe physical stress analysis on the factory floor.
Engineers execute strict ultra-tonnage clamping alignment protocols. By loading the toggle system to its absolute maximum, the team verifies that the massive tie bars stretch evenly and the platens remain perfectly parallel. Simultaneously, the hydraulic manifolds undergo flow-rate stress testing to confirm that the world-class Rexroth valves can sustain massive fluid displacement without internal leakage or pressure drops. This guarantees the equipment is structurally sound before it ever reaches your facility.
Modular Heavy-Freight Logistics
Equipment of this magnitude exceeds standard shipping dimensions and must be systematically dismantled for transport. This requires precise modular heavy-freight securing.
Critical exposed joints and machined surfaces receive an anti-corrosion structural coating to withstand marine environments. The massive frame modules are positioned onto flat rack containers using heavy industrial cranes and locked down permanently with structural steel bracing. A comprehensive modular manifest is verified against every component before vessel departure.
A 12-month warranty activates upon arrival at the destination port. Global engineering teams are available to deploy to your site for heavy reassembly, strict platen realignment, and initial fluid commissioning.
Technical Inquiries
Q1: How does the equipment handle the rapid cooling characteristics of magnesium?
A: Magnesium loses heat extremely fast. When configured as a magnesium die casting machine, the integrated Rexroth hydraulics execute a rapid, massive fluid volume delivery. This ensures the molten alloy completely fills the extensive mold cavity before the temperature drops below the structural threshold.
Q2: Can platen deflection be prevented when casting entire vehicle frames?
A: Platen distortion is the primary cause of flash and mold damage on a very large die casting machine. We engineer oversized platens and perform physical ultra-tonnage clamping alignment during factory testing to ensure the mold faces remain completely sealed under extreme injection forces.
Q3: Is this system capable of producing one-piece automotive structures without porosity?
A: Yes. Operating as a specialized car body making machine, the hydraulic architecture is designed to provide sustained, heavy terminal pressure. This deeply packs the alloy during the final cooling phase, eliminating the internal shrinkage cavities that cause structural failure.
Q4: Why is it critical to specify global standard hydraulic brands for heavy equipment?
A: When casting massive components, a minor hydraulic delay can ruin hundreds of kilograms of alloy per cycle. Using world-class brands like Siemens and Rexroth ensures absolute reliability in fluid dynamics, while also allowing your factory team to source heavy-duty replacement valves from local industrial suppliers immediately.
Hot Tags: ultra-large die casting machine, China ultra-large die casting machine manufacturers, suppliers, factory, aluminum alloy die casting machine, body making machine, car body making machine, magnesium die casting machine, Ultra large Die Casting Machine, very large die casting machine